
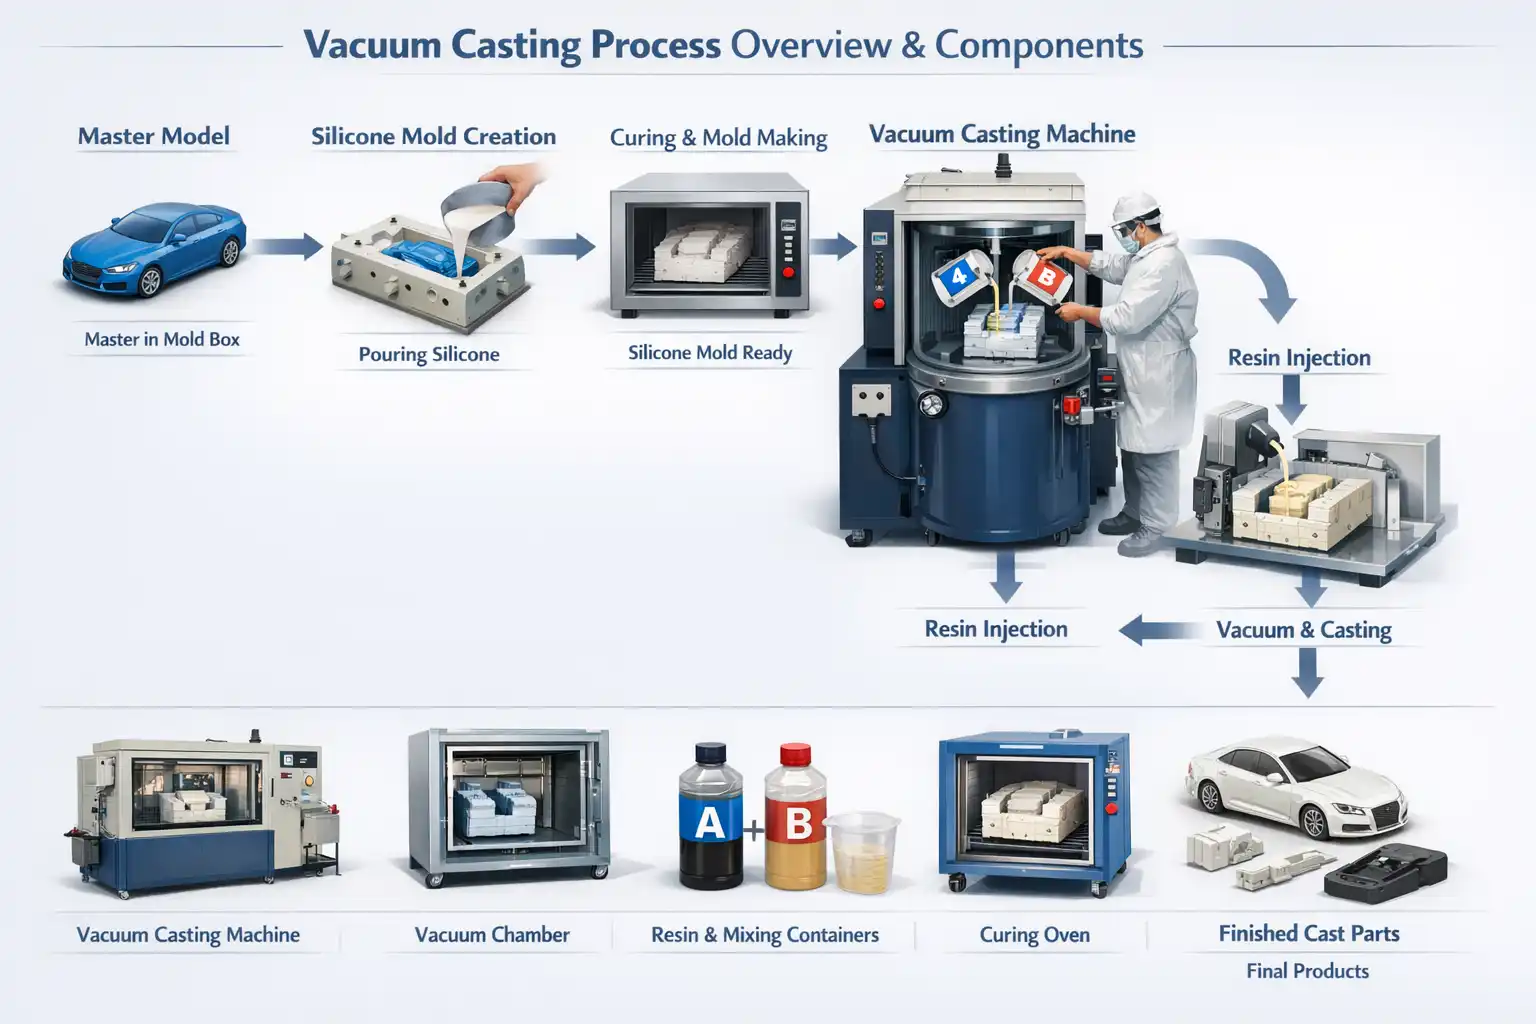
How Does the Vacuum Casting Process Work?
How Does the Vacuum Casting Process Work? From Master Pattern to Finished Parts
Vacuum casting is a practical manufacturing process for producing high-quality prototype parts, functional samples, and low-volume plastic components without the high tooling investment normally associated with Injection Molding. By using a master pattern to create a flexible silicone mold, manufacturers can reproduce multiple parts with consistent geometry, good surface quality, and a wide range of polyurethane materials.
For product developers, engineers, and B2B buyers, understanding the complete vacuum casting process is important when deciding whether the technology is suitable for prototype validation, product testing, presentation samples, or small-batch production. A professional vacuum casting service typically covers the entire workflow, from master pattern preparation and silicone mold making to resin casting, demolding, finishing, and final inspection.
What Is Vacuum Casting Used For?
Vacuum casting is particularly suitable when a project requires more parts than a single prototype but does not yet justify the cost and lead time of hard tooling.
Typical applications include:
Functional prototypes
Product development samples
Plastic housings and enclosures
Automotive prototype components
Consumer electronics parts
Industrial equipment components
Display and presentation models
Engineering validation parts
Assembly and fit-testing samples
Low-volume production parts
Small-batch customized components
For example, a product development team may need 20, 50, or 100 parts for assembly testing, customer evaluation, market testing, or pre-production validation. Manufacturing these parts directly with Injection Molding may require a significant tooling investment. Vacuum casting provides an alternative for producing a limited quantity of parts from a silicone mold.
This makes vacuum casting services especially useful during the transition between prototype development and full-scale production.
The Vacuum Casting Process: From Master Pattern to Finished Parts
Although the exact workflow varies according to part geometry, material, quantity, and quality requirements, a professional vacuum casting project generally follows several controlled stages.
1. CAD Data and Master Pattern Preparation
The process starts with a 3D CAD model supplied by the customer. Engineers first review the geometry to determine whether the part is suitable for silicone molding and vacuum casting.
Important considerations include:
Part dimensions
Wall thickness
Draft and undercut features
Split-line location
Air-trap risks
Required surface finish
Material requirements
Dimensional tolerances
Number of parts required
A master pattern is then manufactured from the approved CAD data. Depending on the project, the master can be produced using CNC machining, 3D printing, or another Precision Manufacturing method.
The master pattern is critical because its surface condition and dimensional accuracy are transferred to the silicone mold and subsequently to the cast parts.
For this reason, the master pattern should be inspected carefully before mold making begins.
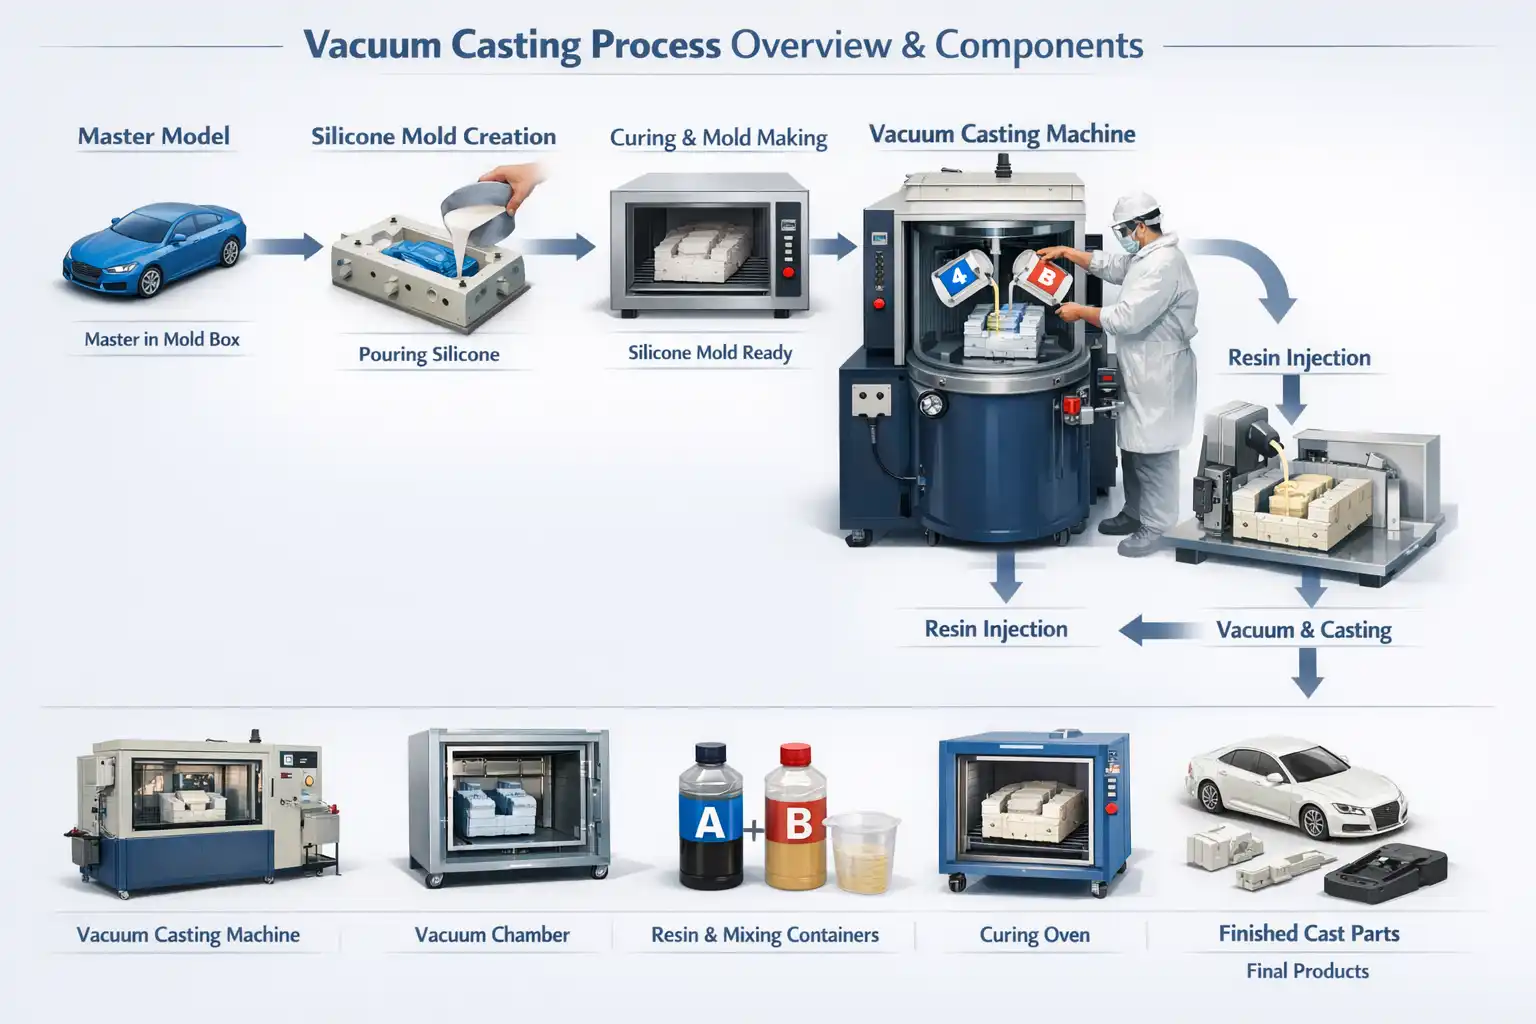
2. Silicone Mold Design and Mold Making
Once the master pattern is approved, it is positioned inside a molding setup and surrounded by liquid silicone.
Before the silicone is poured, engineers determine the appropriate mold split line and establish channels for material filling and air evacuation. Proper mold design is particularly important for complex components containing deep cavities, thin walls, undercuts, or other difficult features.
The liquid silicone is then cured around the master pattern.
After curing, the silicone mold is carefully opened and the master pattern is removed. This creates a flexible negative cavity that reproduces the geometry of the original master.
Unlike a conventional metal Injection Mold, a silicone mold can accommodate certain undercuts and complex geometries because of its flexibility. However, the mold still needs to be designed correctly to minimize deformation and facilitate reliable demolding.
3. Silicone Mold Inspection and Preparation
Before casting production begins, the silicone mold is inspected for defects such as:
Tears
Air bubbles
Incomplete features
Surface damage
Incorrect parting lines
Blocked gates or vents
Dimensional deformation
The mold is then cleaned and prepared for casting.
At this stage, engineers may also adjust the gate and venting arrangement to improve material flow and reduce trapped air.
Good mold preparation is one of the key factors affecting the consistency of subsequent parts.
4. Resin Selection and Preparation
Vacuum casting commonly uses polyurethane-based casting resins because different resin formulations can reproduce different physical characteristics.
Depending on the application, customers may require materials with characteristics similar to:
ABS
PP
PC
PA
Rubber-like elastomers
Transparent plastics
Material selection depends on the intended application rather than simply appearance.
For example, a housing intended for assembly testing may require a rigid resin, while a flexible component may require an elastomeric material. If the parts will undergo functional testing, mechanical properties, temperature resistance, hardness, and other requirements should be considered during material selection.
5. Vacuum Degassing and Resin Mixing
The selected resin components are accurately measured and mixed according to the manufacturer's specifications.
Air trapped during mixing can create bubbles or voids inside the finished part. Therefore, vacuum treatment is used to remove entrapped air before or during the casting operation.
A professional vacuum casting machine provides a controlled environment for this stage. Vacuum pressure, resin temperature, mixing ratio, and processing time need to be controlled according to the material and part geometry.
For B2B production, process control is important because inconsistent mixing or inadequate degassing can result in variations between batches.
6. Vacuum Casting
After preparation, the mixed resin is introduced into the silicone mold under controlled vacuum conditions.
The vacuum environment helps reduce trapped air and allows the resin to fill detailed sections of the mold more reliably. This is particularly useful for parts with complex geometry, thin sections, or fine surface details.
Once the cavity is completely filled, the resin is allowed to cure.
The required curing time depends on the selected material, part size, geometry, and processing conditions.
7. Demolding
After the resin has sufficiently cured, the silicone mold is opened and the finished part is carefully removed.
Because silicone is flexible, the mold can generally be separated from the part without damaging many complex features. However, improper demolding can still cause deformation, tearing, or surface damage.
The part is therefore removed using a controlled procedure rather than simply pulling it from the mold.
8. Trimming, Finishing, and Surface Treatment
The cast part normally requires some secondary finishing.
Excess material around gates, vents, and parting lines is removed. Depending on the customer's requirements, additional operations may include:
Deburring
Sanding
Polishing
Painting
Texture application
Surface coating
Assembly
Logo or marking application
For presentation prototypes, surface finishing can be especially important because the final appearance may need to closely resemble the intended production product.
9. Dimensional Inspection and Quality Control
The final stage is inspection.
Depending on the project requirements, manufacturers may check:
Critical dimensions
Wall thickness
Surface quality
Part weight
Assembly fit
Color consistency
Mechanical characteristics
Visual defects
Batch-to-batch consistency
For engineering applications, inspection data can also be compared with the original CAD model or customer drawings.
This step is important for B2B customers because prototype production is not only about producing a physical model. The parts may be used for engineering decisions, functional testing, customer approval, or preparation for mass production.
Why Is Vacuum Casting Suitable for Low-Volume Production?
One of the major advantages of vacuum casting is its suitability for low-volume production.
Traditional injection molding requires a dedicated hard mold, and tooling costs can become difficult to justify when only a limited number of parts are required.
Vacuum casting uses silicone molds instead, which generally allows manufacturers to move from a finished master pattern to multiple parts without investing in conventional production tooling.
This makes the process useful for:
10–20 prototype parts
Dozens of functional samples
Small-batch production
Pre-production validation
Market testing
Customer samples
Limited product releases
The actual economical quantity depends on part geometry, material, mold life, finishing requirements, and production volume.
For this reason, vacuum casting should not be viewed only as a prototyping technology. For certain projects, it can function as a practical bridge between one-off prototypes and injection molding.
Vacuum Casting for Product Development and Engineering Validation
Another important application is engineering validation.
Before committing to mass production, companies often need physical parts to verify whether the design works as intended.
Vacuum cast parts can be used for:
Fit testing: checking whether components fit correctly with surrounding parts.
Assembly testing: verifying fasteners, interfaces, clearances, and assembly procedures.
Functional testing: evaluating selected mechanical or functional characteristics.
Design validation: identifying problems that may not be visible in a digital CAD model.
Customer evaluation: providing realistic physical samples for approval.
Market testing: producing a limited number of finished-looking products before full production.
This makes vacuum casting particularly valuable during the development stage when design changes are still possible.
Vacuum Casting vs. Injection Molding
Vacuum casting and injection molding serve different production requirements.
Injection molding is generally more appropriate when production volumes are high and the cost of dedicated tooling can be distributed across a large number of parts.
Vacuum casting is often more attractive when the project requires:
Faster prototype production
Lower initial tooling investment
Complex prototype geometries
Small quantities
Multiple material or color variations
Pre-production samples
Short-term or limited-volume production
Therefore, the right question is not whether vacuum casting is better than injection molding in general, but which process better matches the required quantity, performance, lead time, and budget.
What Affects Vacuum Casting Quality?
Several factors determine the final quality of vacuum cast parts.
The first is the accuracy of the master pattern. Any dimensional or surface defect on the master can be reproduced in the silicone mold.
The second is mold design. Poorly positioned gates, vents, or parting lines can increase the risk of air entrapment, flashing, or incomplete filling.
Material preparation is equally important. Incorrect mixing ratios, insufficient degassing, or inappropriate curing conditions can affect mechanical and cosmetic properties.
Finally, production consistency depends on process control. For commercial vacuum casting services, mold condition, resin preparation, vacuum conditions, curing, demolding, and finishing should all be controlled according to the requirements of the project.
When Should You Choose a Vacuum Casting Service?
Vacuum casting is a strong option when you need multiple high-quality plastic parts but do not yet require conventional injection molding tooling.
It is particularly suitable when a project requires:
Functional prototypes
Complex plastic components
High-quality appearance models
Small-batch production
Low-volume manufacturing
Pre-production samples
Engineering validation
Customer approval samples
Market testing parts
For higher production volumes, injection molding may eventually become more economical. For very small quantities or highly customized parts, CNC machining or additive manufacturing may be more appropriate.
The best process depends on the part geometry, material, quantity, dimensional requirements, surface finish, lead time, and intended application.
Conclusion
The vacuum casting process is more than simply pouring resin into a silicone mold. A reliable production workflow requires careful control from CAD data and master pattern preparation through silicone mold making, resin preparation, vacuum casting, curing, demolding, finishing, and final inspection.
For product developers and B2B manufacturers, the main value of vacuum casting is its ability to produce realistic, functional, and repeatable parts without the upfront investment associated with traditional hard tooling. This makes it particularly useful for prototypes, engineering validation, and low-volume or small-batch production.
When selecting a vacuum casting service, buyers should evaluate not only the equipment but also the manufacturer's capabilities in master pattern production, silicone mold design, material selection, process control, finishing, dimensional inspection, and batch consistency. A well-controlled process can provide a practical manufacturing solution between rapid prototyping and full-scale production.